2026 Best Chemical Manufacturing Suppliers for Global Buyers
Choosing the 2026 best chemical manufacturing suppliers requires more than comparing prices or browsing polished websites. Global buyers need evidence, consistency, and practical visibility before approving a new partner. This guide examines suppliers through the realities of the chemical manufacturing industry, including product quality, technical capability, production capacity, regulatory readiness, and delivery performance. A reliable supplier should provide clear specifications, batch records, safety data, and traceable raw material information. These details matter when a shipment crosses borders or supports a sensitive production schedule.
The selection process also considers audited facilities, trained personnel, laboratory controls, and documented quality systems. Strong manufacturers explain how they manage contamination risks, equipment maintenance, worker safety, and environmental responsibilities. Their sales teams should answer technical questions without hiding behind vague promises. Responsiveness matters when a buyer needs a revised specification at 4 p.m. or faces a delayed container at a busy port. Sustainability claims deserve careful review, too. Certifications can help, but independent verification is stronger.
No ranking is flawless. Supplier performance may change with ownership, energy costs, or regional disruptions. Buyers should still conduct their own audits and request current documentation before signing contracts. This overview offers a practical starting point, not a substitute for professional due diligence. It is designed to help procurement teams compare manufacturers with clearer expectations, realistic risk awareness, and greater confidence in long-term cooperation. Some excellent suppliers may remain outside this list. That is worth remembering.
Understanding the Global Chemical Manufacturing Supplier Landscape
The 2026 chemical manufacturing supplier landscape is becoming more regional, specialized, and data-driven. Global buyers now compare production capacity, quality systems, technical support, and delivery reliability together. Price alone rarely explains the real purchasing risk.
A capable supplier should provide clear specifications, recent certificates of analysis, and batch-level traceability. Buyers should review reaction controls, storage conditions, packaging standards, and waste-management procedures. A factory visit can reveal practical details that documents may miss, such as worn equipment or unclear labeling. Small details matter.
Regional supply chains also create different advantages. Producers near major ports may support faster export, while inland facilities may offer stronger access to raw materials. Buyers should examine customs documentation, lead times, emergency inventory, and communication speed. Ask how the supplier handles specification changes. The answer often shows its technical maturity.
No supplier is flawless. Even a well-managed facility may face energy shortages, transport delays, or temporary labor gaps. A careful buyer should test backup plans instead of trusting broad promises. Pilot orders can expose inconsistent viscosity, moisture variation, or damaged packaging before larger commitments. This process takes time. It is still cheaper than correcting a failed shipment. Supplier performance should be reviewed continuously, not only during the first qualification.
Key Criteria for Evaluating Chemical Manufacturers
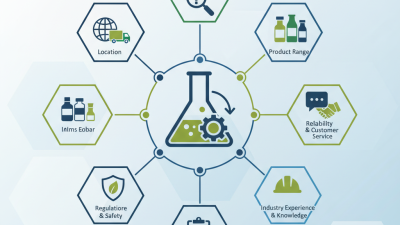
A capable chemical manufacturer should be evaluated on more than price and production capacity.
Buyers need evidence that quality controls work across ordinary and difficult production runs. Ask how the supplier manages raw-material changes, batch records, testing methods, and out-of-specification results. Request sample documentation, such as a certificate of analysis, and check that its measurements match your specifications.
Look closely at traceability.
Can the supplier connect a finished batch to its source materials and production records? Review audit findings, corrective actions, and the process for reporting quality issues. Ask who handles technical questions and how quickly customers receive clear answers. Small details matter. A polished presentation is not proof of consistent performance.
Supply reliability deserves the same scrutiny.
Discuss typical lead times, inventory practices, shipping conditions, and contingency plans for equipment or transport disruptions. Confirm that packaging and product information suit your handling requirements. Where appropriate, arrange a technical review or site assessment before making a long-term commitment. Compare suppliers using the same criteria, not just their quoted prices. Even a thorough review has limits; performance can change, and a checklist cannot replace ongoing communication and periodic reassessment.
Major Product Categories and Their Supply Requirements
Chemical suppliers serve several distinct markets. Basic chemicals, such as acids, alkalis, and solvents, often require steady volumes and clearly defined purity ranges. Specialty chemicals may need tighter batch controls, application testing, or temperature-sensitive handling. Polymers and resins bring different needs: buyers should confirm viscosity, packaging format, and storage life before shipment. Agricultural and water-treatment inputs can require seasonal planning and reliable technical documentation. Small details matter. A drum label that is hard to read can slow receiving checks.
Tips: Request a current specification sheet, safety data sheet, and representative certificate of analysis. Compare the stated test methods, not just the headline purity. Ask how the supplier handles batch variation and delayed shipments. Keep the first order modest when the product is unfamiliar. That may feel cautious, but it can reveal packaging or compatibility issues before larger volumes arrive.
Supply requirements also depend on destination and use. Buyers should discuss container type, pallet configuration, transport conditions, and expected lead times early. Some products tolerate ordinary storage; others need protection from heat, moisture, or light. Confirm that documents match the actual product and shipment, and check whether technical support is available across time zones. A supplier’s capacity figures are useful, but they do not guarantee smooth delivery. I would still verify recent production availability and agree on a practical plan for quality concerns.
2026 Best Chemical Manufacturing Suppliers for Global Buyers
Major product categories and their supply requirements
Approximate global annual production benchmarks for 2023, shown in million metric tonnes. Values represent industry-wide product volumes rather than individual manufacturers or brands.
Sulfuric Acid
Requires corrosion-resistant equipment, dangerous-goods transport, controlled storage, and reliable bulk delivery capacity.
Ammonia
Buyers typically require refrigerated or pressurized logistics, strict safety procedures, and verified hazardous-material documentation.
Ethylene
Supply depends on pipeline, terminal, or specialized shipping access, consistent purity, and long-term volume agreements.
Methanol
Global buyers generally prioritize certified quality, tank-container or bulk-vessel access, and compliance with flammable-liquid regulations.
Caustic Soda
Common requirements include concentration control, compatible packaging, corrosion-resistant handling systems, and dependable regional delivery.
Regional Strengths and Global Reach of Leading Suppliers
Regional strength often determines how reliably chemical suppliers serve global buyers. Local infrastructure matters as much as production capacity.
East Asian manufacturing hubs often provide deep process engineering expertise, dense supplier networks, and efficient container access. European facilities commonly emphasize strict quality systems, traceability, and specialty formulation capabilities. North American producers may offer strong technical support, flexible batch sizes, and dependable research partnerships. These strengths vary by site, not just by region.
In supplier assessments, I look beyond catalog descriptions. I review batch records, audit findings, change-control procedures, and recent delivery performance. A capable supplier should explain how it manages raw material shortages, transport delays, and specification changes. Clear documentation is essential. So is responsive communication.
Global reach depends on more than export experience. Suppliers need regional warehouses, reliable freight partners, and staff who understand local import requirements. Temperature-sensitive materials may require validated packaging and monitored transit. Port access can reduce delays, but it cannot replace careful planning. Some companies appear global while relying on one overloaded facility. That is a risk.
Buyers should compare production locations, backup capacity, quality certifications, and technical response times. Site visits can reveal practical details that brochures hide, such as storage conditions and labeling discipline. No supplier is perfect. Even strong systems need review when regulations, markets, or transport routes change. Supplier selection remains a balance between regional expertise and proven international execution.